WATER & BEVERAGE CAP MOULD
Water Bottle Cap Moulds for High-Volume Production
Mincong manufactures custom injection moulds for water bottle and beverage caps. These tools produce the plastic closure, rather than the bottle or finished caps supplied in bulk. Sealing surfaces, tamper-evident bands and cavity balance are reviewed against your cap drawing and matching bottle neck. We match the runner, cooling and mould size to your cap design, output target and injection machine.
PRODUCTION PRIORITIES
What Matters in a Water Bottle Cap Mould?
For a water bottle cap, the neck finish, seal and tamper-evident band must match the filling line. At higher cavity counts, differences in filling and cooling can affect cap weight and dimensions. The mould review starts with a bottle-neck drawing, cap sample and target caps per hour.
Sealing Consistency
Cap dimensions and sealing surfaces must remain consistent enough to support reliable bottle sealing and capping performance across the production batch.
Tamper-Evident Structure
The band, bridges and post-mould finishing method should be considered early so the moulded cap is compatible with slitting, folding or the selected closure design.
Multi-Cavity Balance
High cavity count increases output only when filling, cooling and ejection remain balanced enough to keep part dimensions and weight under control. For shot-to-shot weight drift, review feed, recovery and transfer in the cap process-control guide.
Cycle Stability
Cycle time should be evaluated together with cooling, machine capacity and cap design. Use our cooling-time and cycle-trial guide to define the timing and acceptance conditions. A fast trial cycle has limited value if it cannot be maintained in continuous production.
Water & Beverage Cap Mould Configuration
The final configuration depends on the closure geometry, production target and injection machine rather than a fixed catalogue specification.
| Mould Type | Custom water bottle cap / beverage cap injection mould |
| Typical Cap Material | PP, PE or project-specific resin |
| Cavity Number | Project-specific; from low-cavity development moulds to high-output multi-cavity solutions |
| Runner System | Hot runner or cold runner according to output, cap weight and investment target |
| Hot Runner Options | YUDO or project-specified system |
| Core / Cavity Steel | H13, S136, 718HH or application-specific selection |
| Mould Base | P20 or specified steel |
| Ejection | Push plate or project-specific ejection structure |
| Critical Dimensions | Defined and verified against the approved cap drawing and inspection plan |
| Service Life | Specified according to steel selection, mould structure, maintenance plan and operating conditions |
| Downstream Process | Can be evaluated together with cap slitting, folding, lining or other auxiliary operations |
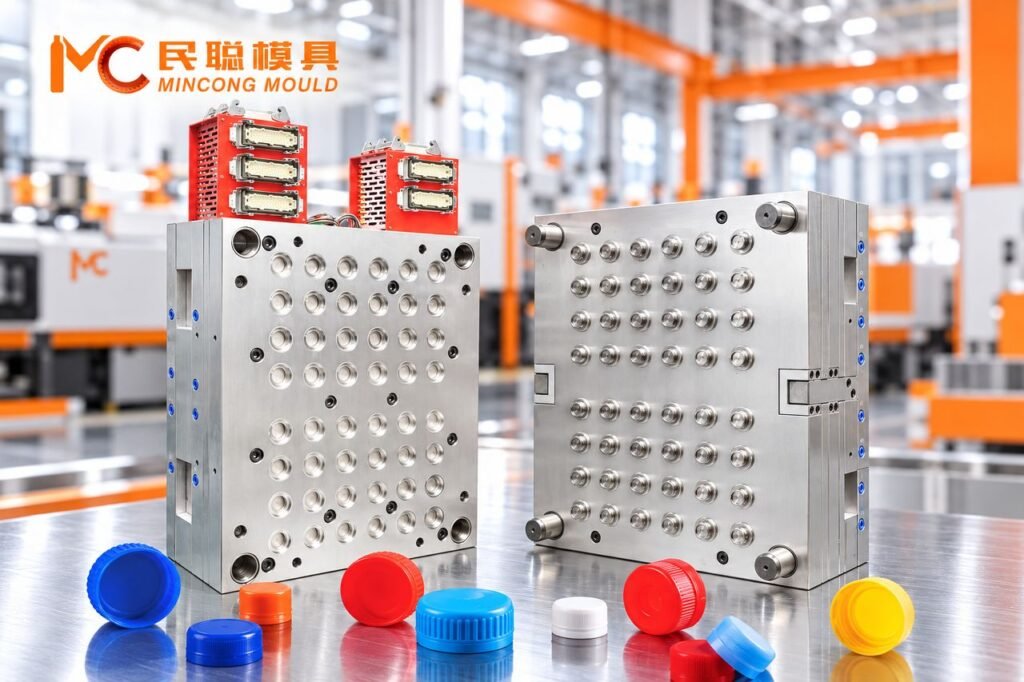
Mould Views and Cap Samples

Multi-cavity tooling views

Water and beverage closure samples
HIGH-OUTPUT DESIGN
Multi-Cavity Water Cap Moulds Need More Than More Cavities
For high-volume water caps, cavity number is only one part of output. Runner balance, cooling consistency, mould size, shot capacity and ejection must remain compatible with the injection machine. A larger mould that forces the machine outside its practical operating range can reduce the benefit of extra cavities.
Cavity count should be matched to the whole production system.
- Target caps per hour
- Machine clamping force
- Shot volume
- Tie-bar spacing
- Mould dimensions
- Cooling capacity
- Automation and downstream handling
Hot Runner or Cold Runner for a Water Cap Mould?
The correct runner system depends on the required output, cap weight, cavity count, machine limits, material usage and maintenance preference. High-volume beverage applications often benefit from a well-balanced hot runner, while a cold runner can still be the practical choice for some lower-output or machine-constrained projects.
Hot Runner Considerations
Material efficiency, filling balance, temperature control, maintenance access and compatibility with the selected cavity layout.
Cold Runner Considerations
Tool simplicity, initial investment, runner handling, machine shot capacity and whether the production target justifies the material trade-off.
TAMPER-EVIDENT PRODUCTION
Design the Cap Mould Together with Slitting and Folding
For tamper-evident water and beverage caps, the mould is only one part of the production route. The bridge design, band geometry and cap condition after moulding should match the intended slitting or folding process. Considering the auxiliary process early can reduce later adjustment work.
Designed Around Your Injection Machine
Before finalising the water cap mould, we recommend checking the actual injection machine instead of assuming a standard machine condition.
- Clamping force
- Tie-bar spacing
- Maximum mould dimensions
- Mould height range
- Opening stroke
- Shot capacity
- Nozzle radius
- Locating ring diameter
- Ejector stroke
- Available automation interfaces
Typical Water & Beverage Cap Applications
Mineral Water Caps
Closure geometry and neck finish are reviewed for repeatable sealing and high-volume capping.
Purified Water Closures
Cavity balance and cooling are considered alongside the specified bottle and line speed.
Juice and Beverage Caps
Material, cap design and product handling determine the appropriate runner and finishing route. When an approved resin grade changes, qualify the replacement grade before correcting the tool to suit its first trial.
Tamper-Evident Closures
Band and bridge features are evaluated with any slitting or folding step after moulding.
Beverage Closure Examples
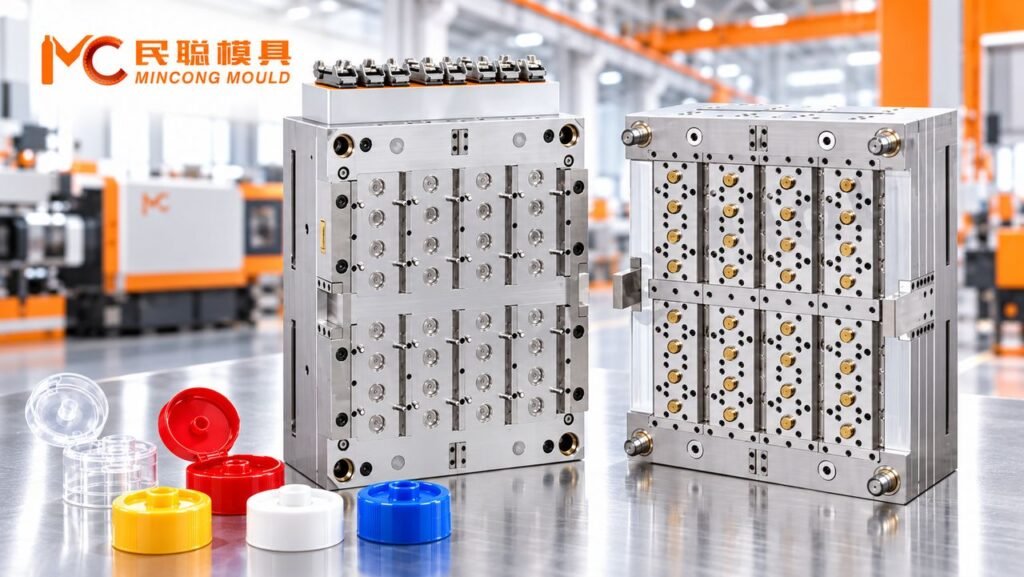
Mould with finished cap designs

Closer view of the mould faces
What We Need to Evaluate Your Water Cap Project
- Cap sample or 2D / 3D drawing
- Bottle neck / closure matching information
- Cap material
- Target production capacity
- Required cavity number, if already defined
- Injection-machine model and specifications
- Hot runner or cold runner preference, if any
- Tamper-evident slitting / folding requirement
- Cap weight or lightweighting target, if relevant
- Any sealing, ejection or production issue the new mould should improve
FAQ
Water Cap Mould FAQs
How many cavities should a water cap mould have?
There is no universal cavity number. It should be matched to the required caps per hour, cap size, machine tonnage, shot capacity, mould dimensions, runner system and cooling capability.
Is a hot runner necessary for a high-cavity water cap mould?
Not in every project, but high-output multi-cavity production often benefits from the material efficiency and flow control of a properly designed hot runner. The machine and investment conditions still need to be checked. Read our hot runner vs cold runner cap mould guide to compare the production considerations, and our injection-machine compatibility checklist to prepare the machine data.
Can you design the mould for an existing injection machine?
Yes. We recommend checking the machine’s clamping force, tie-bar spacing, shot capacity, mould-height range, nozzle, locating ring and opening stroke before finalising the mould.
How is a tamper-evident band handled after moulding?
The downstream route depends on the cap design. Some closures require slitting, folding or other finishing steps. We can evaluate the cap mould together with the intended auxiliary process.
What affects water cap mould life?
Steel selection, heat treatment, mould structure, cooling, moving components, maintenance and actual production conditions all influence service life.
Water & beverage cap mould videos
Selected videos from our project archive. Each clip relates to its own tooling or product example. Select Play to load the YouTube player.
Water cap mould trial
Archive video from Mincong Mould’s YouTube channel.
Watch on YouTube ↗Multi-cavity cap mould
Archive video from Mincong Mould’s YouTube channel.
Watch on YouTube ↗Sports cap mould trial
Archive video from Mincong Mould’s YouTube channel.
Watch on YouTube ↗If the mould produces polymer strands at the gate, use the hot-runner stringing solutions before changing the runner configuration.
PRODUCT SHOWCASE
Explore Related Packaging Moulds
Explore related tooling for your packaging project. Each page explains its own scope and quotation requirements.
 Concept illustration
RELATED PRODUCT
Sports Cap Moulds for Push-Pull and Drinking-Spout Closures
Review sports cap moulds around spout movement, sealing, assembly and release. Send component drawings, resin grades and machine data for tooling review.
Explore product →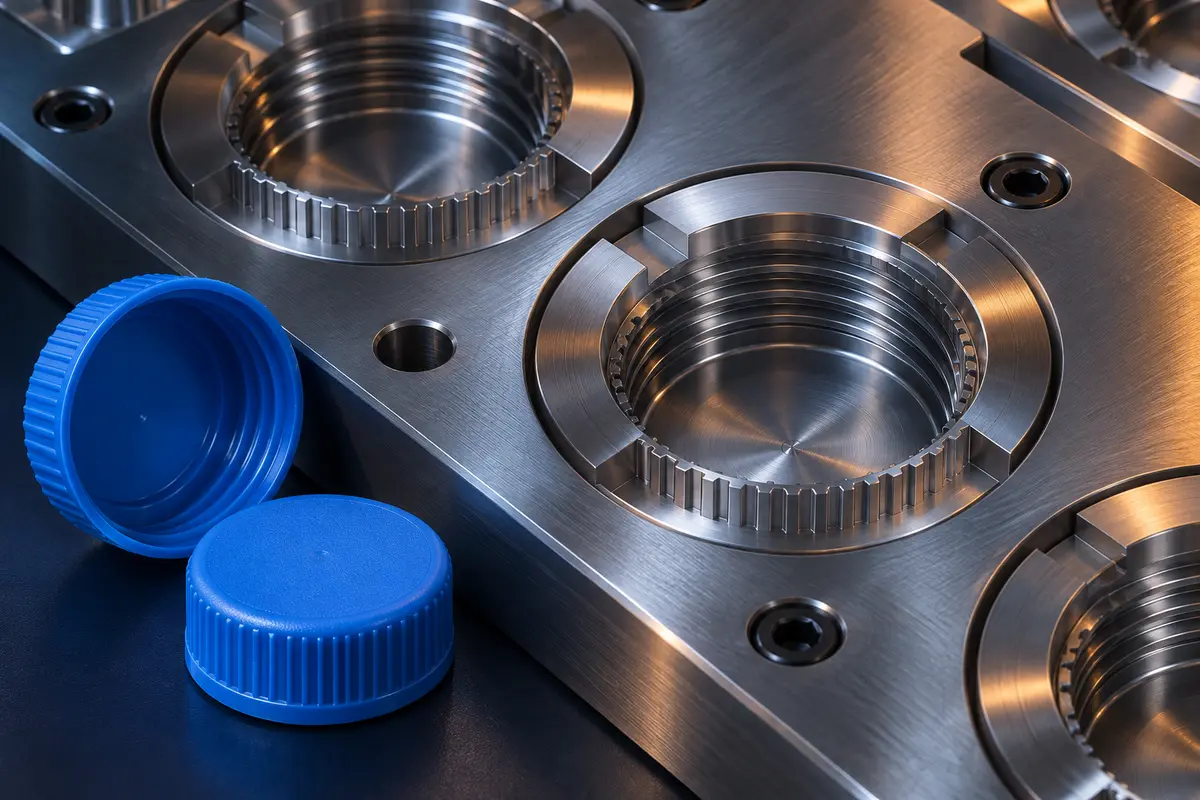
32-Cavity Water Bottle Cap Mould
Compare cavity insert and integral plate options for water cap production.
Explore product →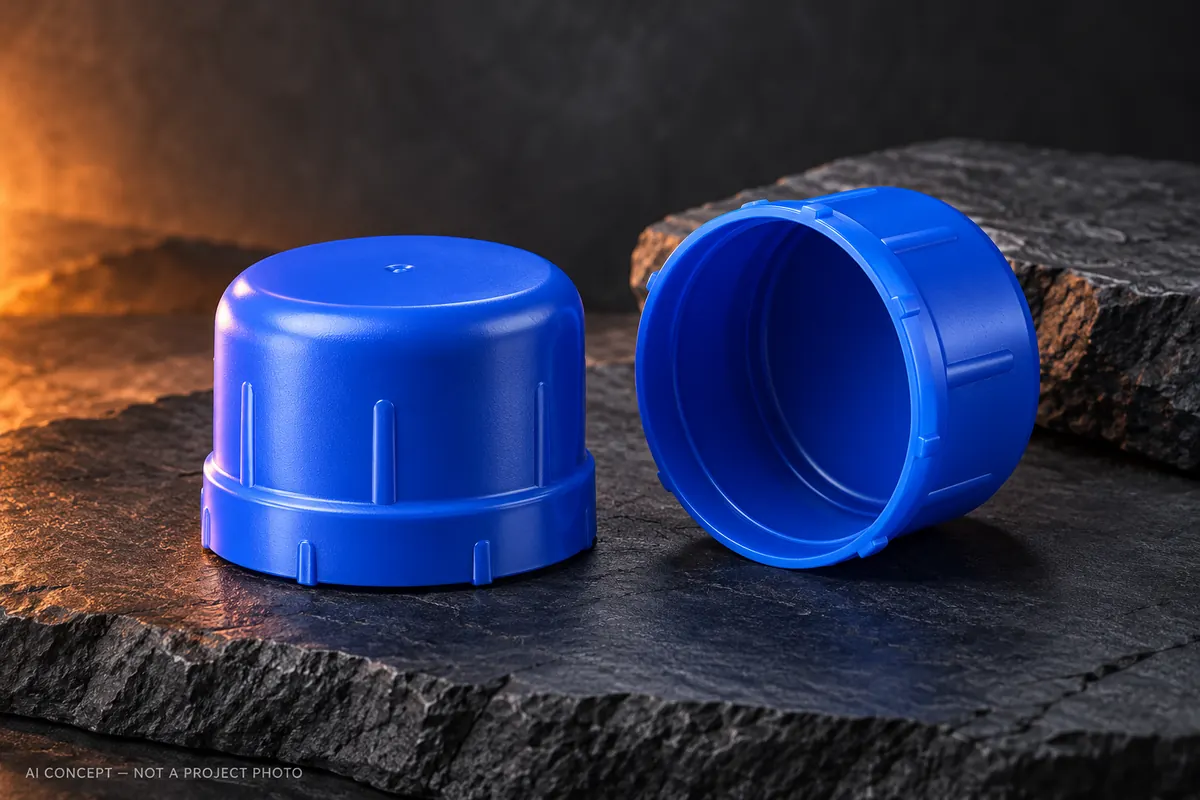 Concept illustration
RELATED PRODUCT
5 Gallon Water Cap Moulds for Bottle and Dispenser Fit
Define a 5 gallon water cap mould around the bottle neck, sealing components and dispenser interface. Review tooling scope, release and trial requirements.
Explore product →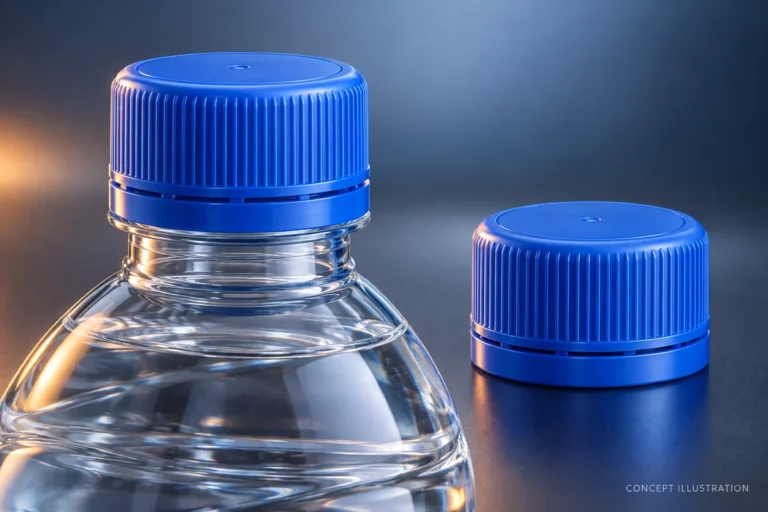 Concept illustration
TAMPER-EVIDENT WATER CAP MOULDS
Tamper-Evident Water Cap Moulds
Review the bottle neck, seal, tamper band and downstream process as a defined closure project.
Explore product →
FUNCTIONAL CLOSURES
Oil & Functional Closure Moulds
Explore tooling for oil caps, dispensing features and defined opening arrangements.
Explore product →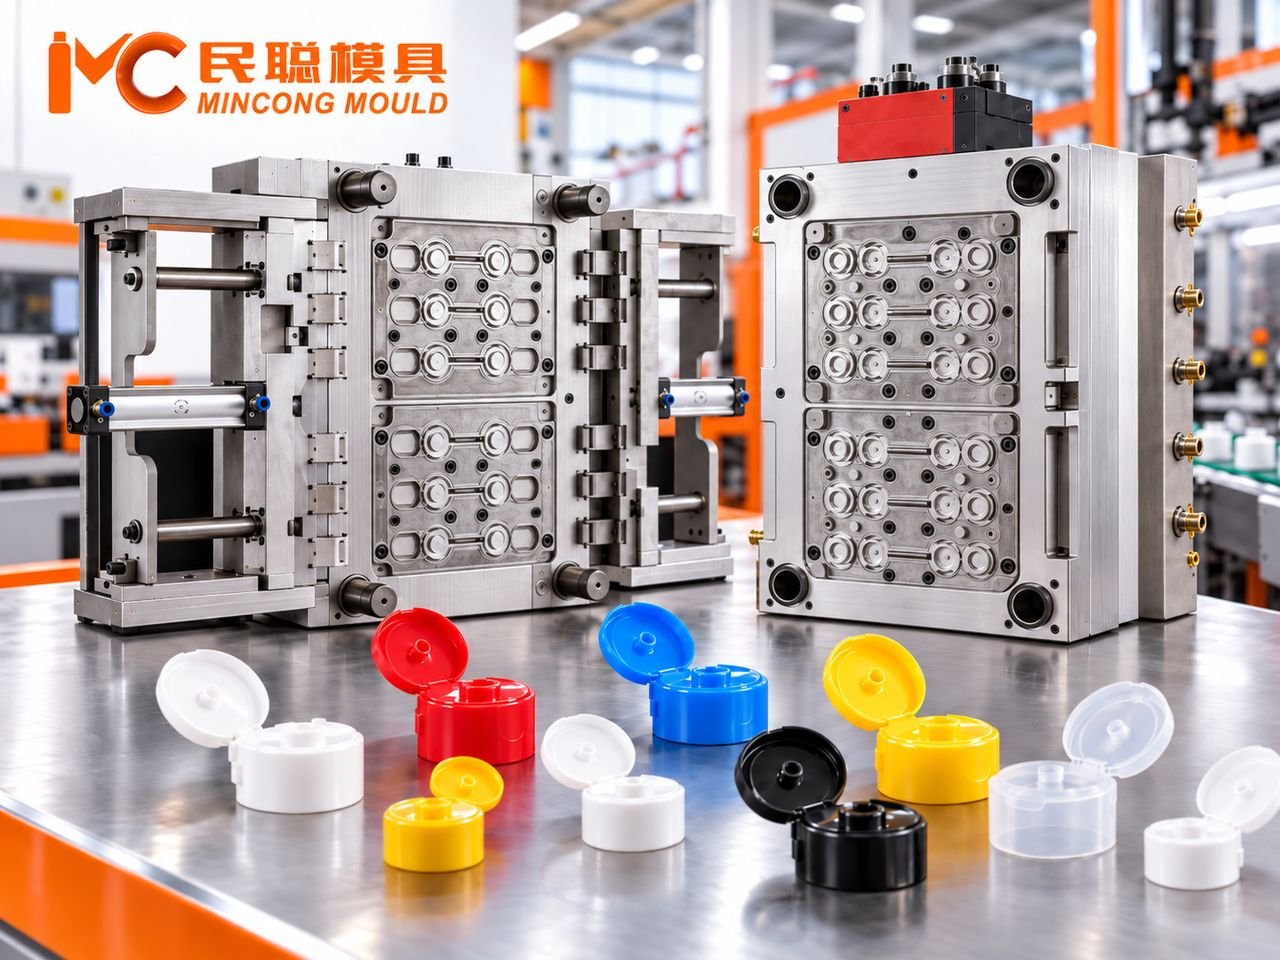
HINGED CLOSURES
Flip Top Cap Moulds
Explore tooling for a one-piece hinged closure and its closing requirements.
Explore product →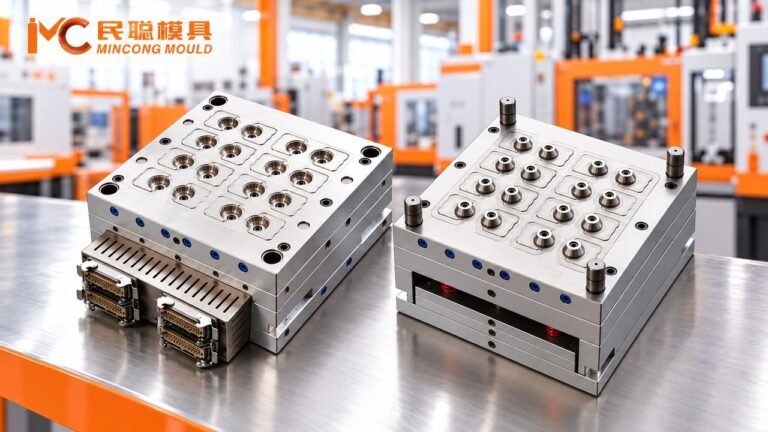
CONTAINER HANDLES
Handle Moulds
Review handle tooling around container fit, load requirements and release.
Explore product →Planning a Water or Beverage Cap Project?
Send the cap sample or drawing together with your injection-machine information and target output. We can evaluate the cavity layout, runner system and downstream process before you commit to tooling.