Short shots in injection molding are incomplete parts caused by a cavity not filling completely. For a plastic cap, the missing material may appear at a skirt edge, a lid detail or another feature. The first useful question is where the incomplete region occurs—and whether that pattern repeats across cavities and over time.
A short-looking cap also needs identification: confirm that material was never formed there, rather than being torn away during release or handling. Keep a complete reference beside the affected specimen. This article focuses on incomplete filling; the cap defect trial-record guide covers the shared record format for other concerns.
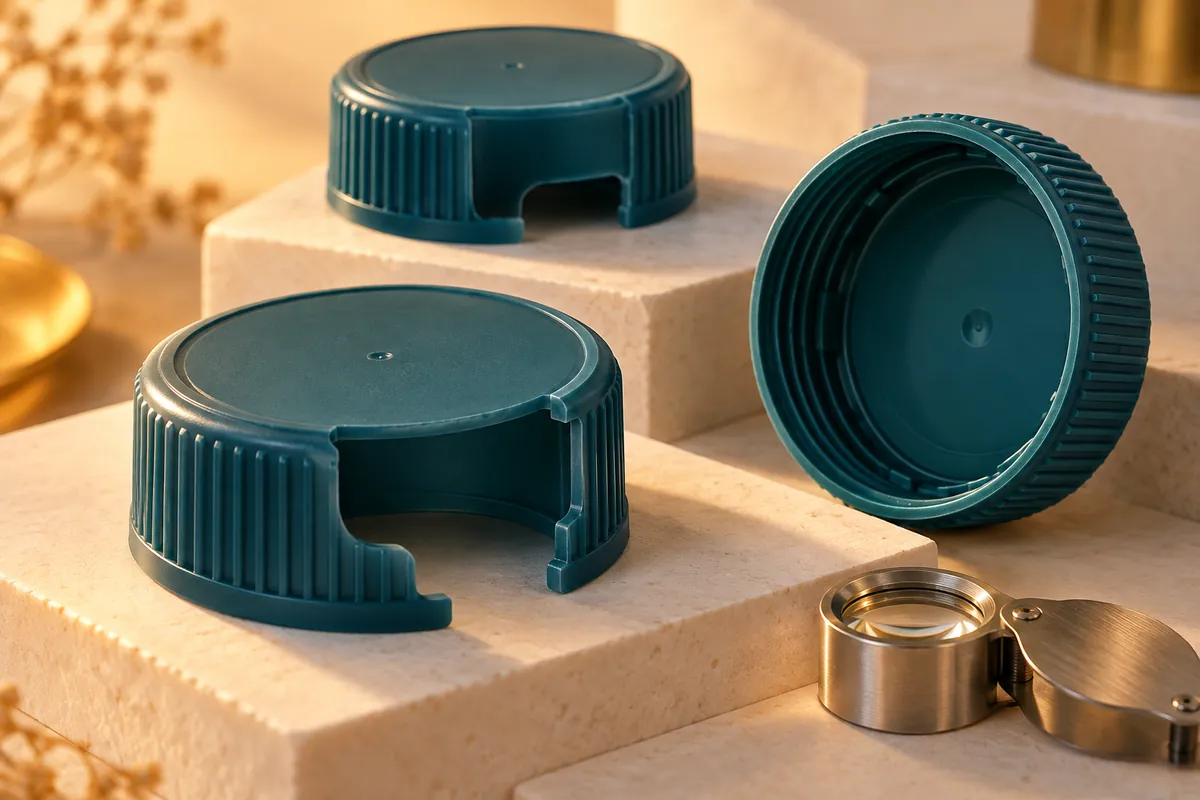
Preserve the cavity pattern before changing the setup
Collect samples in a way that keeps cavity and shot identity intact. A bag containing mixed incomplete caps loses information that could distinguish a local concern from a change affecting the whole mould.
Record the resin grade, colour system, mould and machine references, drawing revision and trial stage. Identify whether the samples came from startup, a stable run or a restart. Add a whole-part photo and a close-up of the missing region under consistent lighting.
Use the following table to plan the next review. The patterns are investigation leads, not diagnoses.
| Observed pattern | Useful comparison | Questions to investigate |
|---|---|---|
| Many cavities become incomplete together | The last accepted shot and the associated machine record | Did material delivery, filling conditions or a shared system condition change? |
| One cavity or a local group repeatedly differs | Identified affected and accepted cavities from the same shots | Is there a local flow-path, temperature, gate or venting difference? |
| The same small feature remains unfilled | Feature location relative to the flow route and surrounding geometry | Is filling hesitating or meeting a restriction or trapped air? |
| The concern appears after a stop or restart | Sequence of samples and recorded recovery conditions | What changed between the accepted run and the restarted condition? |
For example, suppose a hypothetical multi-cavity trial produces an incomplete lid edge at one identified position. Preserve the other cavities from the same shots. Raising every temperature immediately would remove the baseline before explaining the local difference.
Check material delivery and the filling record together
Autodesk's short-shot guidance identifies several possible contributors: restricted or hesitant flow, trapped air, thermal conditions, insufficient material delivery and machine faults. This range is why a photograph alone cannot select the correction.
Ask the process team to compare the accepted and affected runs. Useful records can include the shot settings, transfer condition, filling time, pressure information and cushion, where available and relevant. Keep the actual machine units with the values; a percentage displayed on one machine is not automatically comparable with another machine's setting.
Include material-feed interruptions or reported delivery irregularities in the discussion. The aim is to determine what the machine actually delivered and under which conditions, rather than treating a saved recipe name as proof that nothing changed.
These are suggested comparison fields. They are not instructions to increase pressure, temperature or shot size without assessing the material, machine and tooling limits.
Separate a flow-path concern from a brand assumption
Where the pattern points toward a local area, identify the path from the machine nozzle through the runner and gate to the incomplete feature. Our sprue, runner and gate guide explains the terminology. Ask which inspection or process evidence would test the suspected restriction.
For a hot-runner tool, retain the installed system and controller references, zone identification, available temperature records and relevant alarms. With valve gating, include the applicable actuation record if it is part of the investigation.
For a YUDO installation, use the matching system documentation rather than a general description of “a YUDO hot runner.” If a Husky system is being considered for a future project, confirm its configuration and supply scope separately. Husky's official manual directory and YUDO's manual portal are reference routes; neither brand name diagnoses an incomplete cap or proves that a particular configuration is installed.
Consider venting and local geometry before approving steel changes
Air that cannot escape can oppose cavity filling. A recurring incomplete area near an end-of-fill region is therefore worth discussing with the tooling and process teams. It does not establish a blocked vent from the photograph alone.
Identify the relevant venting provision and its condition. Keep routine inspection or cleaning separate from permission to alter vent dimensions, a gate or the plastic part. A steel change needs a defined location, reason and follow-up checks.
For PP processing, the INEOS Polypropylene Processing Guide lists both process and mould-related areas for short-shot investigation. Its historical guidance is a technical reference, not a substitute for the current resin-grade recommendations or the installed equipment manual.
A controlled filling study may help the process team understand the flow pattern. If proposed, ask for its method, sample identification and limitations. Intentionally incomplete study samples must remain separate from production acceptance samples.
Close the trial with complete, functional caps
Choose a documented next action based on the evidence and retain before-and-after samples. Where practical, isolate the change so its effect remains interpretable. If several changes must occur together, record the full package.
Then check the original acceptance requirements. A visually complete cap can still need dimensional, sealing, engagement or hinge checks. Filling the missing area is one result; approving the closure requires the relevant functions as well.
For a water and beverage cap mould or flip-top cap mould, include the affected feature and sample pattern when requesting support. Use the mould review form with the available drawings and trial records. A clear comparison helps the engineering discussion reach a testable next step.
Questions buyers often ask
Does a short shot always mean the injection machine is too small?
No. Machine capability is one area to review, alongside material delivery, flow restrictions, thermal conditions and venting. Confirm the evidence for the proposed cause.
Should injection pressure always be increased first?
No. The suitable action depends on the limiting condition. An adjustment can create another problem, so the process team should evaluate the whole result rather than judging only whether the missing region fills.
Is a complete cap enough to approve the correction?
It confirms that the observed incomplete region has been filled on that specimen. Agreement on cavity coverage, repeatability and the applicable package-function checks is still needed.