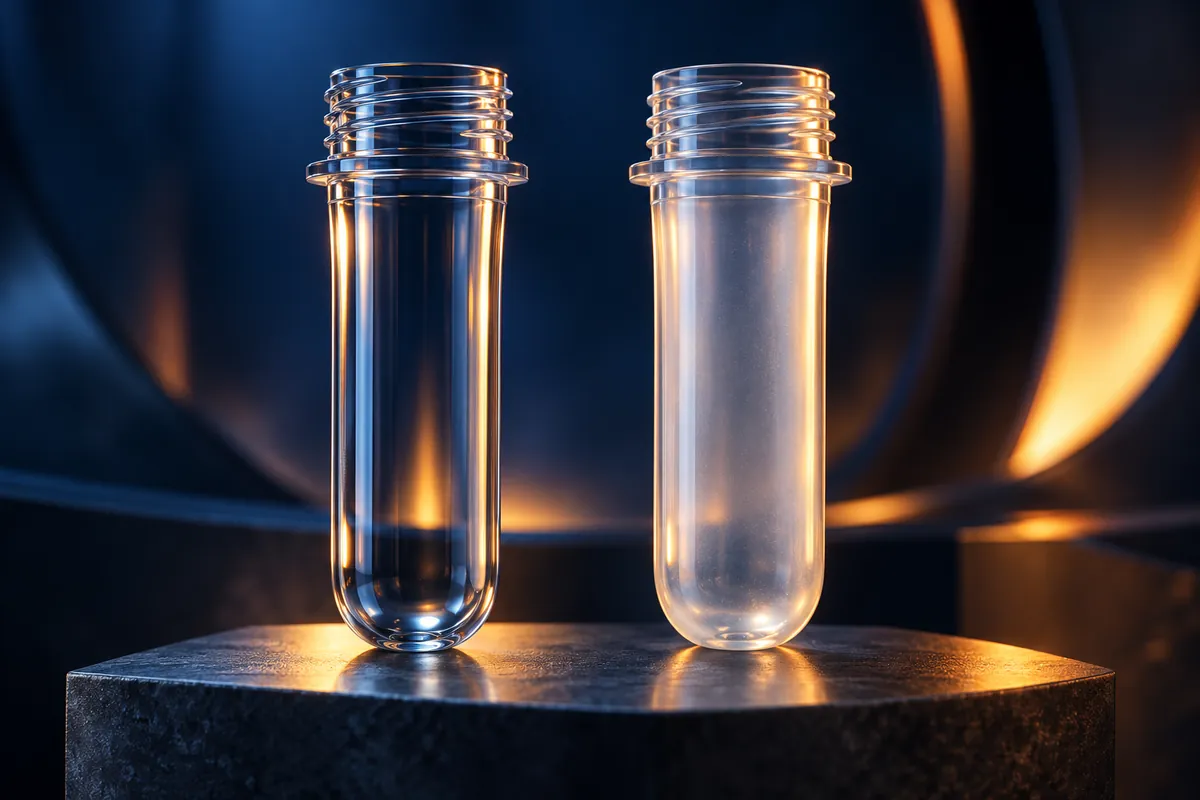
If a PET preform remains cloudy after material preparation meets its specified requirement, investigate where the optical change develops before choosing a temperature correction. Restore the relevant cooling or melt condition and prove the result in the defined preform and bottle programme. A white region is a symptom, not independent evidence of crystallinity or moisture damage.
Establish that the symptom belongs to the preform stage
Inspect preforms before reheating and blowing, using consistent lighting and sample condition. If the cloudiness only becomes visible after blowing, the downstream process belongs in the investigation. Do not alter preform steel solely because the final bottle looks hazy.
Distinguish a body-wide optical change from a local gate-region mark, a surface scratch or a feature visible only on one side. Preserve cavity identity. The pattern helps choose a test but does not by itself identify a material mechanism.
Close the material-preparation question, then move on
Confirm the actual resin grade and that the agreed material-readiness checks represent the feed entering the machine. Use the separate drying guide if that requirement is not met. Avoid repeatedly raising the dryer setting when the material route has not been shown to be at fault.
Include recent grade, colour or blend changes in the comparison. A clarity target must be evaluated for that specific material and package; a supplier's claim for one resin family is not a blanket approval of another feedstock or mixture.
Restore the intended local heat removal
Where cloudiness is concentrated in a recurring region or cavity, check whether the corresponding cooling arrangement works as designed. Resolve an identified blockage, connection error or inadequate flow through the approved maintenance route. More nominal cooling time cannot reliably replace a circuit that is not performing its intended function.
Compare the required thermal condition with the actual release and handling sequence. If the preform is removed or handled before its defined condition is achieved, review that sequence as part of the correction. Do not assume that a visually acceptable neck proves that every part of the body has received adequate cooling.
Compare melt uniformity without adopting a universal heat direction
The Mold-Masters PET manual includes both material-preparation and process checks in its haze guidance, including melt preparation and cooling. Its suggested actions belong to a specific system context. The useful principle is to test the suspected limitation, not to apply every temperature or screw-setting change in the list.
If evidence points to incomplete melt uniformity, compare an appropriate process adjustment within the actual grade and equipment guidance. If the concern is excessive thermal exposure or inadequate heat removal, a different action may be needed. Do not increase heat or shear indefinitely to improve an optical result while disregarding material condition.
Keep a local repair local until the evidence changes
After a cavity insert or cooling connection is serviced, a new cloudy region in that cavity warrants a check of the changed circuit and forming interface. Verify the actual branch condition; an acceptable chiller-panel display does not independently establish flow through that branch. Restore an identified fault before raising temperatures across otherwise acceptable cavities.
If the concern appears only after the preforms enter the bottle process, preserve representative preforms and bottles from the same comparison. Review the reheat and blowing conditions with that process owner. Correcting the bottle stage and correcting the preform tool are different decisions, even when the final optical symptom looks similar.
Accept restored clarity alongside the package requirements
Use the agreed appearance reference and compare samples after the same conditioning. Carry the selected preforms through the specified bottle process where that is part of acceptance. Assess the other required dimensions and functions so that improved clarity does not conceal another problem.
Where a decision depends on crystallinity, intrinsic viscosity or another material property, arrange the appropriate test with a competent facility. Photographs alone cannot establish those values. The corrective trial should answer one defined question and retain the approved material and tooling reference until the result supports a change.
Send the resin identity, defect stage, cavity and location pattern, relevant material-readiness evidence and current cooling arrangement when requesting a review. These inputs help separate a drying fault, a local tooling issue and a wider production-system limitation without promising that one setting will solve every cloudy preform.
Related engineering resources
- PET Preform Mould
- PET Preform Drying Problems: Correct the Material Route Before Raising Heat
- PET Preform Cooling: Define the Cycle Before Comparing Mould Proposals
- PET Preform Hot Runner: Agree Gate Quality Before the Trial
Technical references and scope
- Mold-Masters — PET-Series User Manual, section 9.2.12 Haze
- Eastman — grade-specific clarity and qualification support
Supplier examples describe their own products. They do not establish Mincong certification, supplier affiliation or a validated project result. Proposed checks must be agreed for the specific component, resin and production equipment.